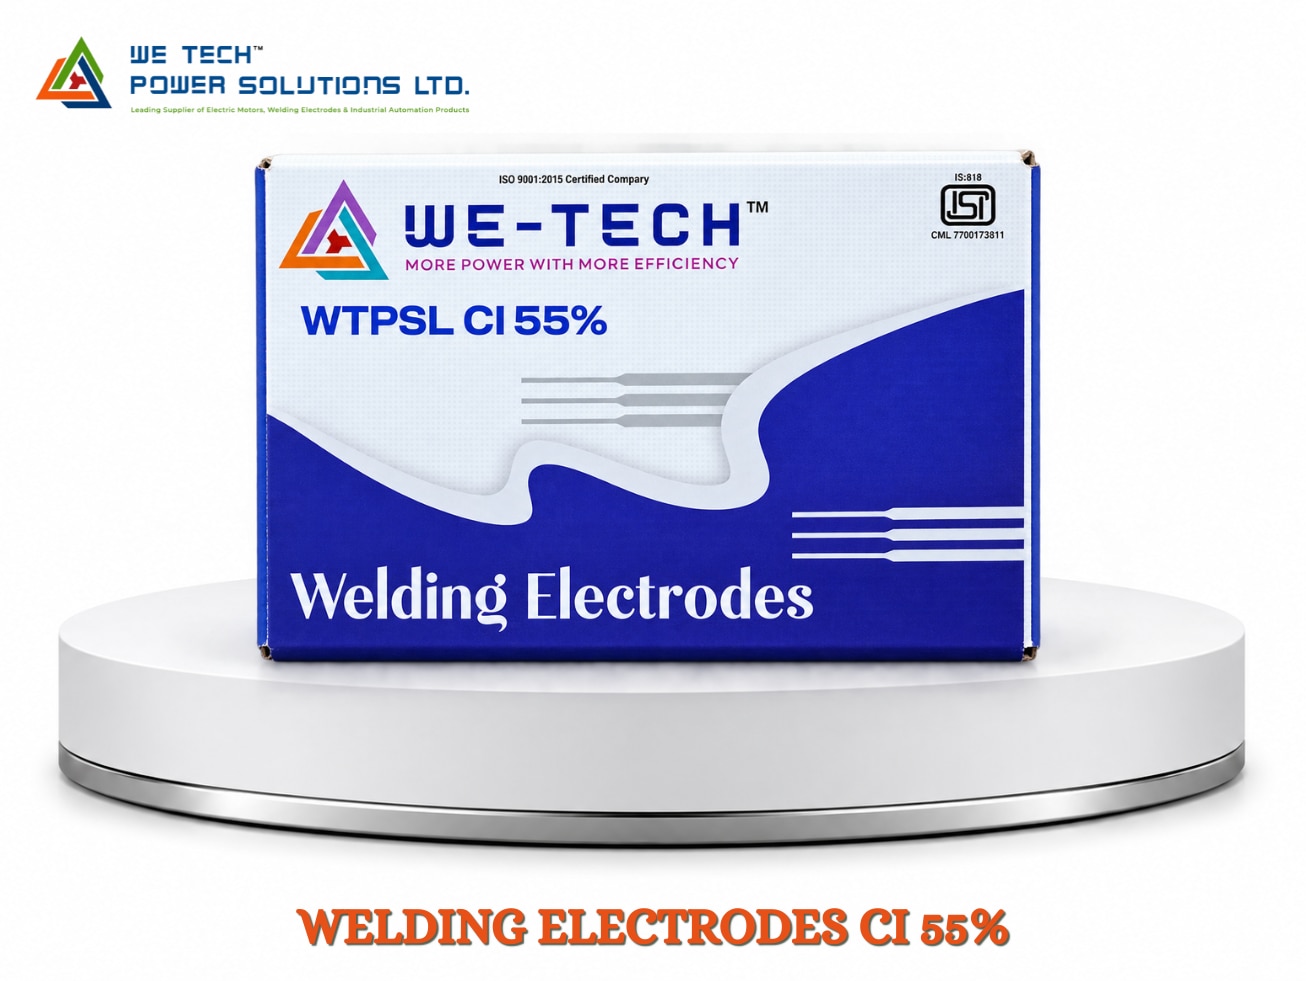
WELDING ELECTRODES CI 55%
Description
Welding Electrodes CI 55% Trader in Ahmedabad.
We, Tech Power Solutions Ltd, supply CI 55% Welding Electrodes in Ahmedabad for cast iron repair, maintenance, and fabrication applications. This medium-heavy coated, basic-type, all-position electrode contains approximately 55% nickel and is designed to produce weld metal with good strength, ductility, and machinability. Its hydrogen-controlled formulation makes it suitable for repairing different cast iron components and joining cast iron with steel.
Technical Specifications
• AWS Classification: AWS A / SFA 5.15: ENiFe-CI
• Electrode Type: Ni-Fe Type
• Coating: Medium-Heavy, Basic Type
• Welding Position: All Positions
• Identification: Name Printed
• Weld Deposit: Machinable
• Dilution: Controlled
• Penetration: Controlled
Key Features of CI 55% Welding Electrodes
As a welding electrode CI 55% Supplier in Gujarat, We Tech Power Solutions Ltd offers a Ni-Fe type electrode developed for controlled dilution and penetration. The electrode has a machinable weld deposit and can be used for ductile, malleable, and grey cast iron. It can also be used when the exact cast iron composition is unknown or difficult to identify, provided suitable welding procedures are followed.
Applications of CI 55% Welding Electrodes
For customers looking for a Welding Electrodes CI 55% Dealer in Saudi Arabia, these electrodes can handle a range of cast iron maintenance and repair jobs. Typical applications include repairing broken heavy castings, transmission housings and couplings, foundry defects, cast iron-to-steel joints, and machining corrections. Follow proper joint preparation and welding procedures based on the component and repair requirements.
Common Applications
• Repair of broken heavy castings
• Transmission housings and couplings
• Foundry defect repair
• Joining cast iron to steel
• Machining corrections
• Repair of ductile, malleable and grey cast iron
Chemical Composition
The Welding Electrodes in Bahrain range has the following reference chemical composition: carbon at 1.2%, nickel at 54%, and copper at 0.5%. Nickel-iron electrode chemistry is an important consideration when selecting a consumable for cast iron because the weld deposit needs to suit the base material and the intended repair or joining application.
· Carbon: 1.2%
· Nickel: 54%
· Copper: 0.5%
Mechanical Properties
The Welding Electrodes CI 55% reference data specifies a hardness of 150–190 BHN in the as-welded condition. This information can help evaluate the expected machinability and finishing requirements of a repaired cast iron component. Actual welding results can depend on the base material, joint preparation, welding technique, and operating conditions.
· Property: Hardness
· Value: 150–190 BHN
Recommended Current Settings
For CI 55% welding electrodes, the reference current range varies by electrode diameter. The specified settings are 70–110 A for 3.15 mm, 90–120 A for 4.0 mm, and 180–240 A for 5.0 mm electrodes. Adjust the actual current selection according to the welding position, joint condition, equipment, and applicable welding procedure.
· Electrode Diameter: 3.15 mm — Current Range: 70–110 A
· Electrode Diameter: 4.0 mm — Current Range: 90–120 A
· Electrode Diameter: 5.0 mm — Current Range: 180–240 A
Why Choose We Tech Power Solutions Ltd?
We Tech Power Solutions Ltd provides welding consumables for industrial repair, fabrication, and maintenance requirements. When selecting a cast iron electrode, consider factors such as base-metal type, component thickness, joint design, machinability requirements, and welding position to achieve a suitable repair.
Contact We Tech Power Solutions Ltd for CI 55% welding electrodes and discuss your cast iron welding and repair requirements.
Top 3 FAQs
1. What is CI 55% welding electrode used for?
CI 55% electrodes are designed for cast iron repair and joining applications, including heavy castings, housings, couplings, foundry defects, and cast iron-to-steel joints.
2. What type of electrode is CI 55%?
It is a Ni-Fe type, basic-coated, all-position electrode classified as AWS A/SFA 5.15: ENiFe-CI.
3. What is the hardness of the CI 55% weld deposit?
The reference specification gives an as-welded hardness of 150–190 BHN.